

Paints Coatings Adhesives
Industrial Solvents & Monomers Supplier for Global Manufacturing
Gnee Bioical is a professional supplier of industrial solvents, monomers, and chemical intermediates widely used in the paints, coatings, inks, adhesives, and resin manufacturing industries.
These materials play a critical role in:
- Coating formulation and film formation
- Resin dissolution and viscosity control
- Adhesive performance optimization
- Polymer synthesis and modification
- Industrial surface treatment and cleaning processes
We provide stable bulk supply with complete export documentation including COA, MSDS, and TDS, supporting global chemical distributors and manufacturing companies.


Product advantages and features
Gnee Bioical supplies high-quality industrial solvents, monomers, and intermediates widely used in paints, coatings, and adhesives manufacturing.
Stable Industrial Grade Quality
Consistent purity and batch-to-batch stability suitable for large-scale production.
01
Strong Application Compatibility
Excellent compatibility with acrylic, epoxy, polyurethane, and vinyl resin systems.
02
Controlled Physical Properties
Stable evaporation rate, solvency strength, and viscosity control performance.
03
Export-Ready Quality System
Full documentation support including COA, MSDS, and TDS for global compliance.
04
Flexible Industrial Supply
Available in drums, IBC tanks, and ISO tanks for global logistics requirements.
05
Product Type
In industrial chemistry, raw materials for coatings and adhesives are generally divided into four categories:
Solvents (Active & Dilution Agents):Used to dissolve resins and adjust viscosity, drying rate, and film formation behavior.
Monomers (Polymer Building Blocks):Used to produce acrylic, vinyl, and other polymer resins.
Chemical Intermediates:Used as upstream feedstocks in resin and polymer production.
Functional Additive Solvents:Used to improve coating performance, adhesion, leveling, and processing stability.
Our Products
Industrial solvents, monomers, and intermediates for paints, coatings, and adhesives manufacturing.

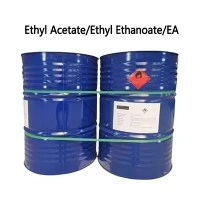
Ethyl Acetate (EA, CAS 141-78-6)
Fast-evaporating solvent widely used in coatings, inks, and adhesives due to excellent solvency and drying performance.

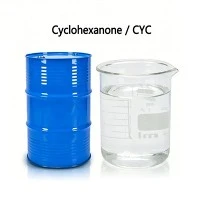
Cyclohexanone (CYC, CAS 108-94-1)
High-performance polar solvent used in PVC systems, adhesives, and advanced coating formulations.

Methyl Methacrylate (MMA, CAS 80-62-6)
Key monomer for acrylic resins used in coatings and adhesives.

Dichloromethane (DCM, CAS 75-09-2)
Strong solvent used in adhesives, paint stripping, and industrial cleaning.

N,N-Dimethylacetamide (DMAC, CAS 127-19-5)
High-boiling polar solvent for polyurethane and polymer systems.

Glacial Acetic Acid (GAA, CAS 64-19-7)
Key intermediate for VAM production used in adhesives and coating resins.
Industrial Applications
Our raw materials are widely used in:
Industrial coatings (anti-corrosion, marine, protective coatings)
Architectural paints and decorative coatings
Printing inks (flexographic, gravure inks)
Adhesives and sealants (PU, acrylic, solvent-based systems)
Resin and polymer manufacturing
Surface treatment and industrial cleaning systems
Packaging Solutions
We provide a full range of flexible and UN-certified export packaging solutions designed to comply with global ocean, road, and rail transport regulations, as well as diverse industrial production and storage requirements.
All chemical packaging is designed to be leak-proof, pressure-resistant, and stackable, ensuring safe handling, long-distance international transportation, and efficient warehouse storage.
Standard Packaging Options
- 190 kg UN-approved galvanized steel drums
Corrosion-resistant and explosion-proof, widely used for flammable and hazardous liquid chemicals in international export markets.
- 200 kg HDPE plastic drums
Acid- and alkali-resistant with high chemical stability, suitable for corrosive liquid chemicals and contamination-sensitive products.
- 1000 kg IBC tote tanks
Forklift-compatible intermediate bulk containers designed for efficient loading, unloading, and cost-effective medium-volume industrial use.
- ISO tank containers
Ideal for bulk liquid transportation, offering the most economical solution for large-volume and long-term supply contracts.
Customized Packaging & Labeling Services
We offer flexible customization based on customer and regulatory requirements, including:
- Customized drum capacity
- Private brand labeling (OEM service)
- GHS-compliant hazard labels
- Waterproof packaging film
- Batch number and country-of-origin marking
- Customized outer packaging color and design
All customization is designed to comply with local customs regulations and end-user factory requirements.
Packaging Compliance & Safety Advantage
All packaging solutions comply with international chemical transport regulations, including:
- IMDG Code (Sea Transport)
- ADR Agreement (Road Transport)
- IATA DGR (Air Transport)
Each packaging unit is:
- Fully labeled with standardized hazard markings
- Accompanied by complete shipping documentation
- Tested for airtightness and leakage prevention before shipment
This ensures safe loading, handling, transit, and long-term storage in global logistics environments.

Automobile manufacturing

Automobile manufacturing

Automobile manufacturing

Automobile manufacturing

Automobile manufacturing

Automobile manufacturing
Company Advantages
Stable Industrial Supply
Long-term production capability ensures continuous bulk supply.
Strict Quality Control
Each batch is tested before shipment with consistent quality assurance.
Complete Documentation
COA (Certificate of Analysis)
MSDS (Material Safety Data Sheet)
TDS (Technical Data Sheet)
Global Export Experience
Support for sea freight, rail transport, and multimodal logistics.
Flexible Cooperation Models
Support traders, distributors, OEM manufacturers, and long-term contracts.
Third-Party Inspection
SGS or equivalent inspection available upon request.
FAQ
Q: What are the main chemicals used in paints, coatings, and adhesives?
A: The most commonly used raw materials include industrial solvents, resins, additives, and curing agents. Typical solvents such as Cyclohexanone, Ethyl Acetate, and Acetone help dissolve resins and adjust viscosity for better application performance.
Q: Why are industrial solvents important in coating formulations?
A: Industrial solvents play a key role in controlling viscosity, drying speed, and film formation. They ensure smooth application, improve leveling, and reduce coating defects such as bubbles, cracking, or uneven surfaces.
Q: What is the role of Cyclohexanone in coatings and adhesives?
A: Cyclohexanone is a high-boiling ketone solvent with strong solvency for acrylic, epoxy, vinyl, and nitrocellulose resins. It is commonly used to improve flow, leveling, and stability in industrial coating systems.
Q: What makes a solvent suitable for industrial paint production?
A: A suitable industrial solvent should have stable evaporation rate, strong resin compatibility, low moisture content, and consistent purity. These properties ensure stable production performance and high-quality coating results.
Q: Are these chemicals suitable for bulk industrial procurement?
A: Yes. Industrial-grade solvents and coating chemicals are typically supplied in bulk packaging such as drums, IBC tanks, or ISO tanks. Stable supply, batch consistency, and COA documentation are critical for large-scale procurement.
Q: What quality standards are required for coating raw materials?
A: Industrial coating chemicals are generally required to meet international quality systems such as ISO manufacturing standards and provide COA (Certificate of Analysis) for each batch to ensure traceability and consistency.
Q: How is product quality ensured in industrial chemical supply?
A: Quality is ensured through controlled production processes, distillation or purification technology, and third-party laboratory testing. Each batch should be traceable via COA and meet specified technical parameters.